06.11.2024
Precision takes shape
Machining solutions for scroll compressors
MAPAL harnesses both its knowledge about components and the market to deliver optimal machining solutions to the automotive industry in the field of electromobility. Global developments, trends and drivers are incorporated into its solution portfolio for critical components like the scroll compressor.
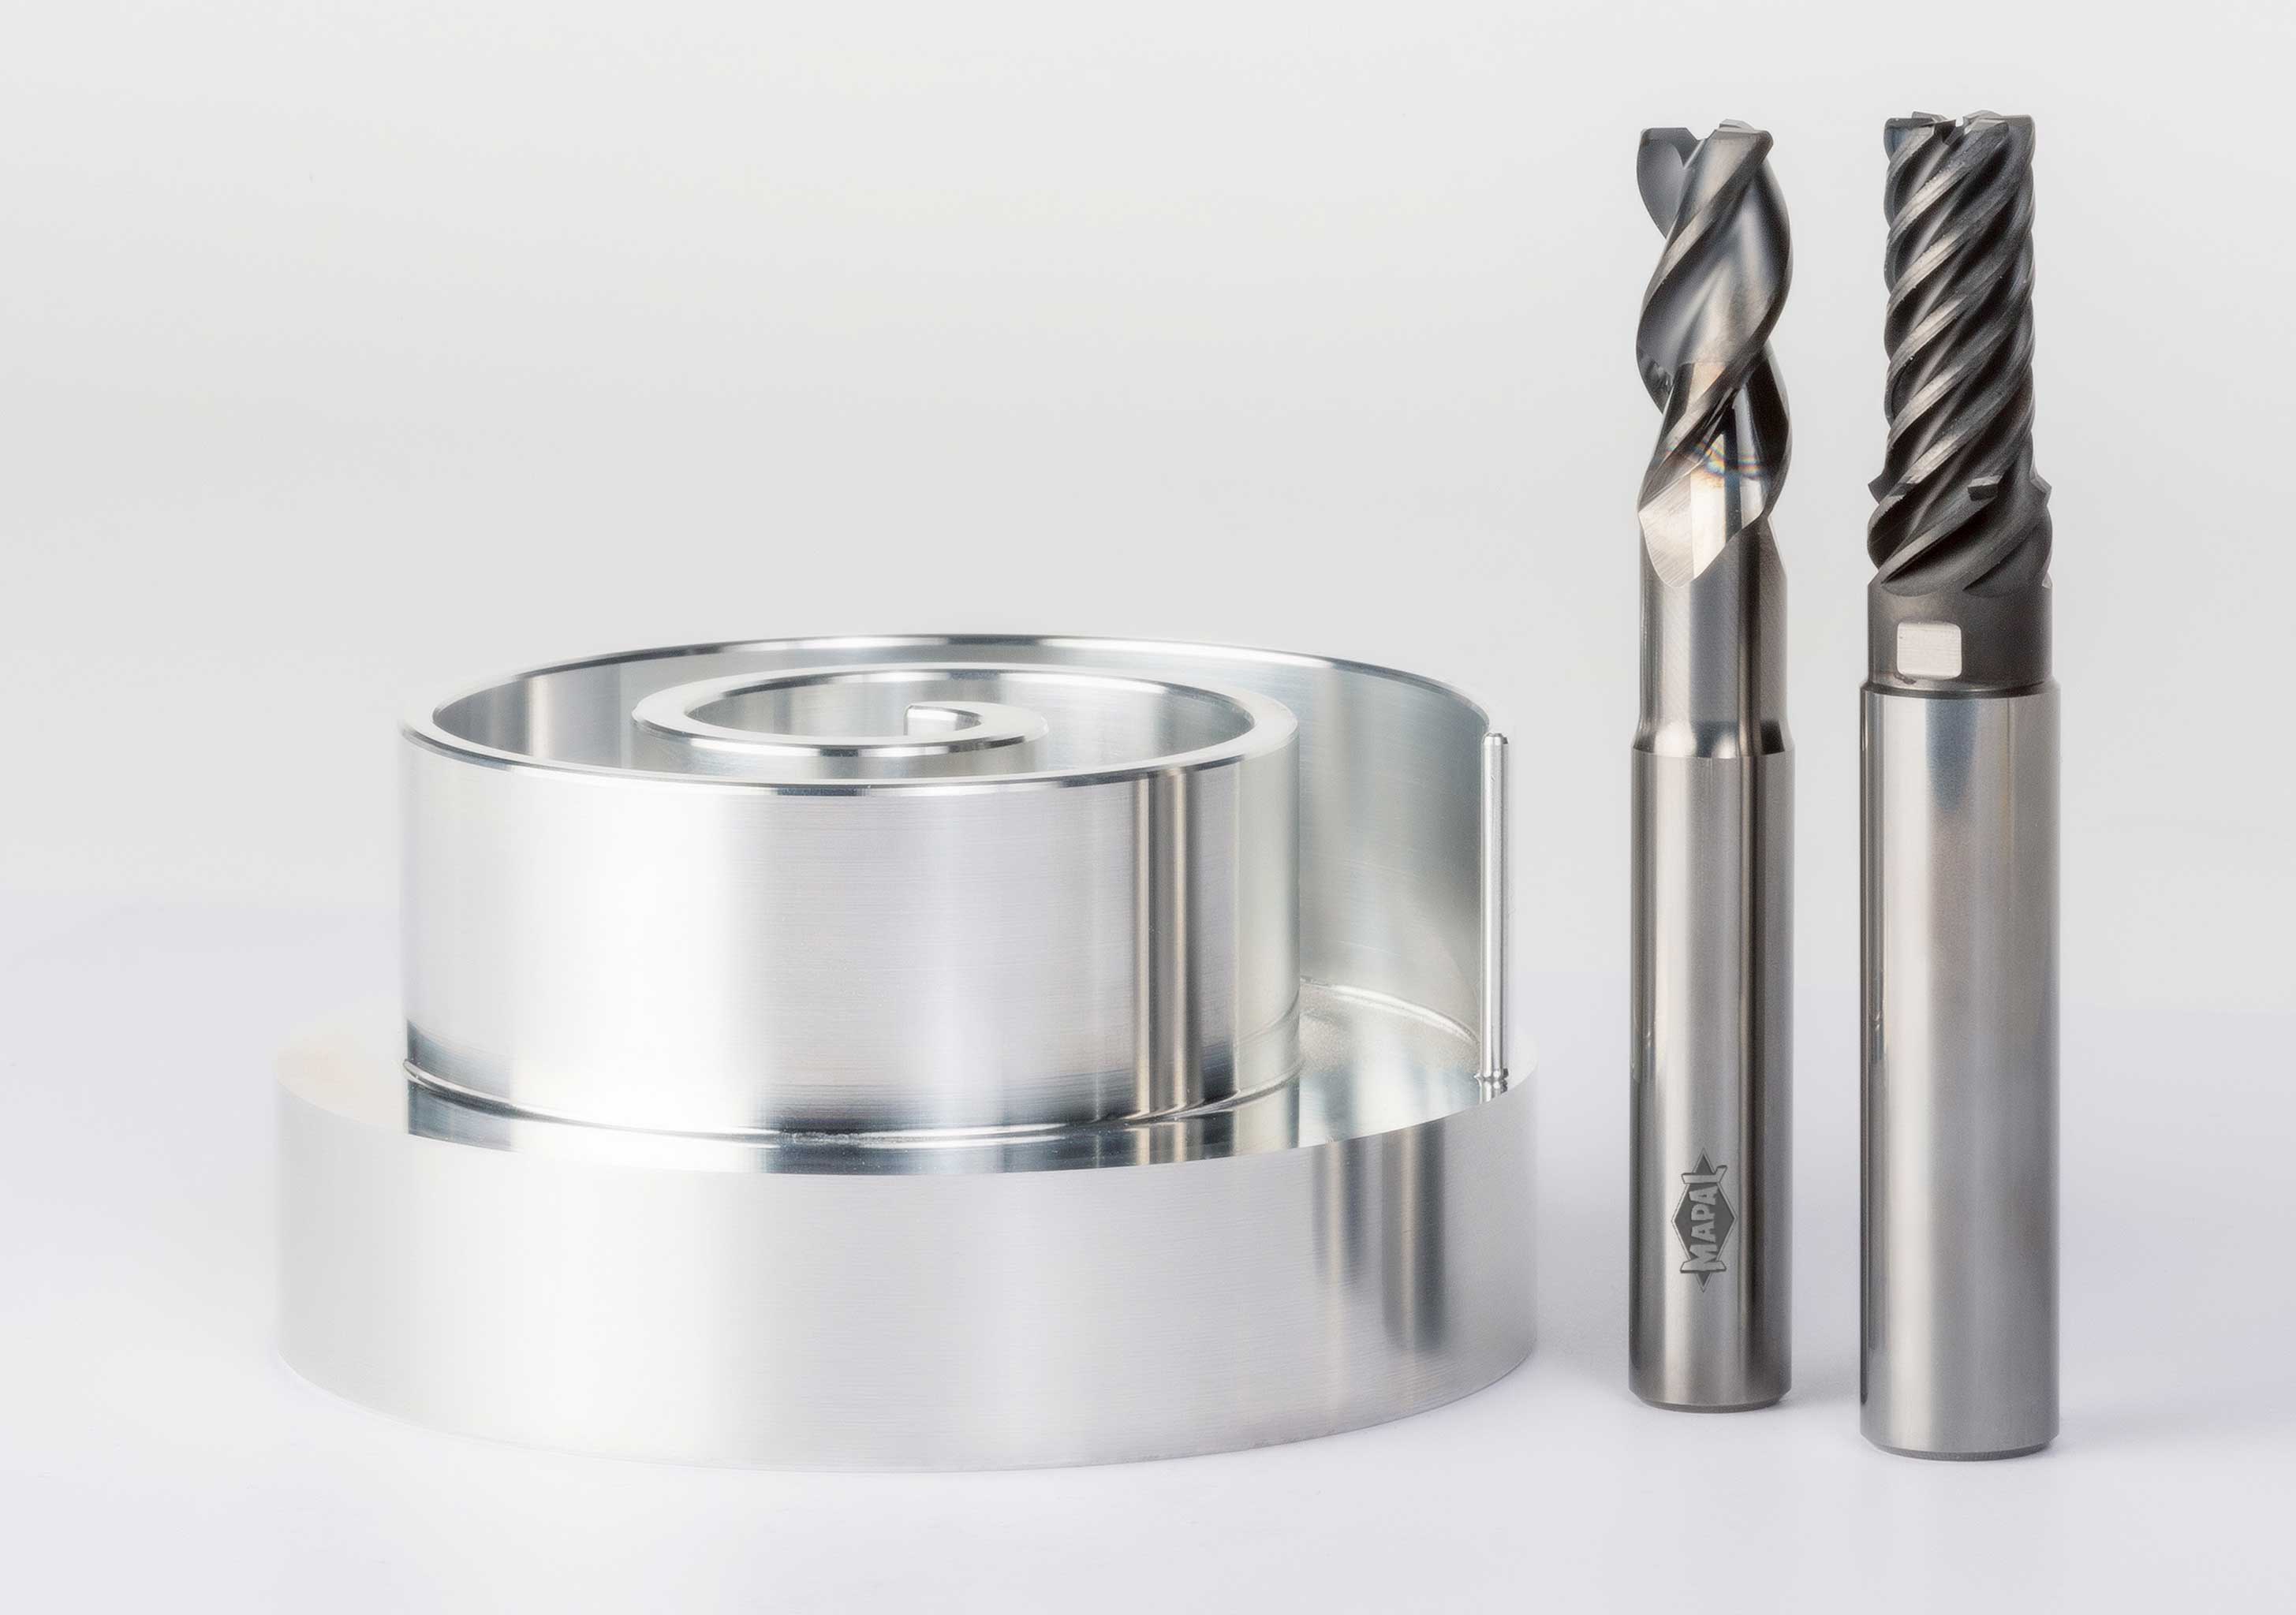
Scroll compressor is required as a focus component with high quantities
MAPAL has defined the scroll compressor as a critical component in the field of electromobility. It has very high demands with respect to the machining quality and is required in high quantities. With specifications that are sometimes less than 20 µm, the form of the scroll spirals and perpendicularity have very tight tolerances. A surface finish with an average roughness depth in the single micrometre range is required for the flawless functionality of both spirals in relation to one another.
The machining process to manufacture the scrolls involves milling the surfaces of the spiral shapes as well as the top and base surfaces. The pre-machining process already comes very close to the final contour. A step milling cutter provides the finish for the face surface and spiral shapes during the fine machining that follows. In a single stroke, the tool moves inwards, turns around at the innermost point with the smallest radius, and then moves outwards again along the other side of the spiral shape. Special radii and transitions between the face surface and spiral call for extremely precise contours on the milling tool.
Hohe Standzeit trotz extremer Schärfe
Die Fräserschneide muss so gewählt werden, dass einerseits die verlangte Form exakt umgesetzt wird, andererseits hohe Standzeiten erreicht werden. Bei den derzeit am häufigsten eingesetzten Aluminiumwerkstoffen AlSi1 und AlSi12 schafft ein Finishfräser von MAPAL mehr als 2.000 Bauteile. Bei der Vorbearbeitung achten die Spezialisten aus Aalen darauf, so wenig Aufmaß wie möglich stehen zu lassen, aber so viel wie notwendig, um einen sicheren Prozess abbilden zu können. Der Fräser schneidet die Oberfläche mit geringen Kräften, anstatt diese zu drücken und zu verformen.
Vor allem in der Schlichtbearbeitung gibt es mehrere Lösungsoptionen, die den Anforderungen entsprechend eingesetzt werden können. MAPAL geht in der Projektauslegung schematisch nach der Basic-, Performance- und Expert-Klassifizierung vor.
Um erste Prototypen zu fertigen und in den Tests einzusetzen, kann auf Basic-Lösungen mit Standardwerkzeugen zurückgegriffen werden. Auf der Stufe Performance kommen Sonderwerkzeuge mit Konturgeometrie für das Bauteil ins Spiel. Im Fokus der Expert-Lösungen stehen neben der exakten Konturbearbeitung vor allem maximale Standzeiten für möglichst effiziente Prozesse in der Großserie, wofür auch spezielle Beschichtungen eingesetzt werden. Ein dreischneidiges Werkzeug mit Diamantbeschichtung ist dabei für Aluminiumlegierungen mit höherem Silizium-Anteil das Maß der Dinge.
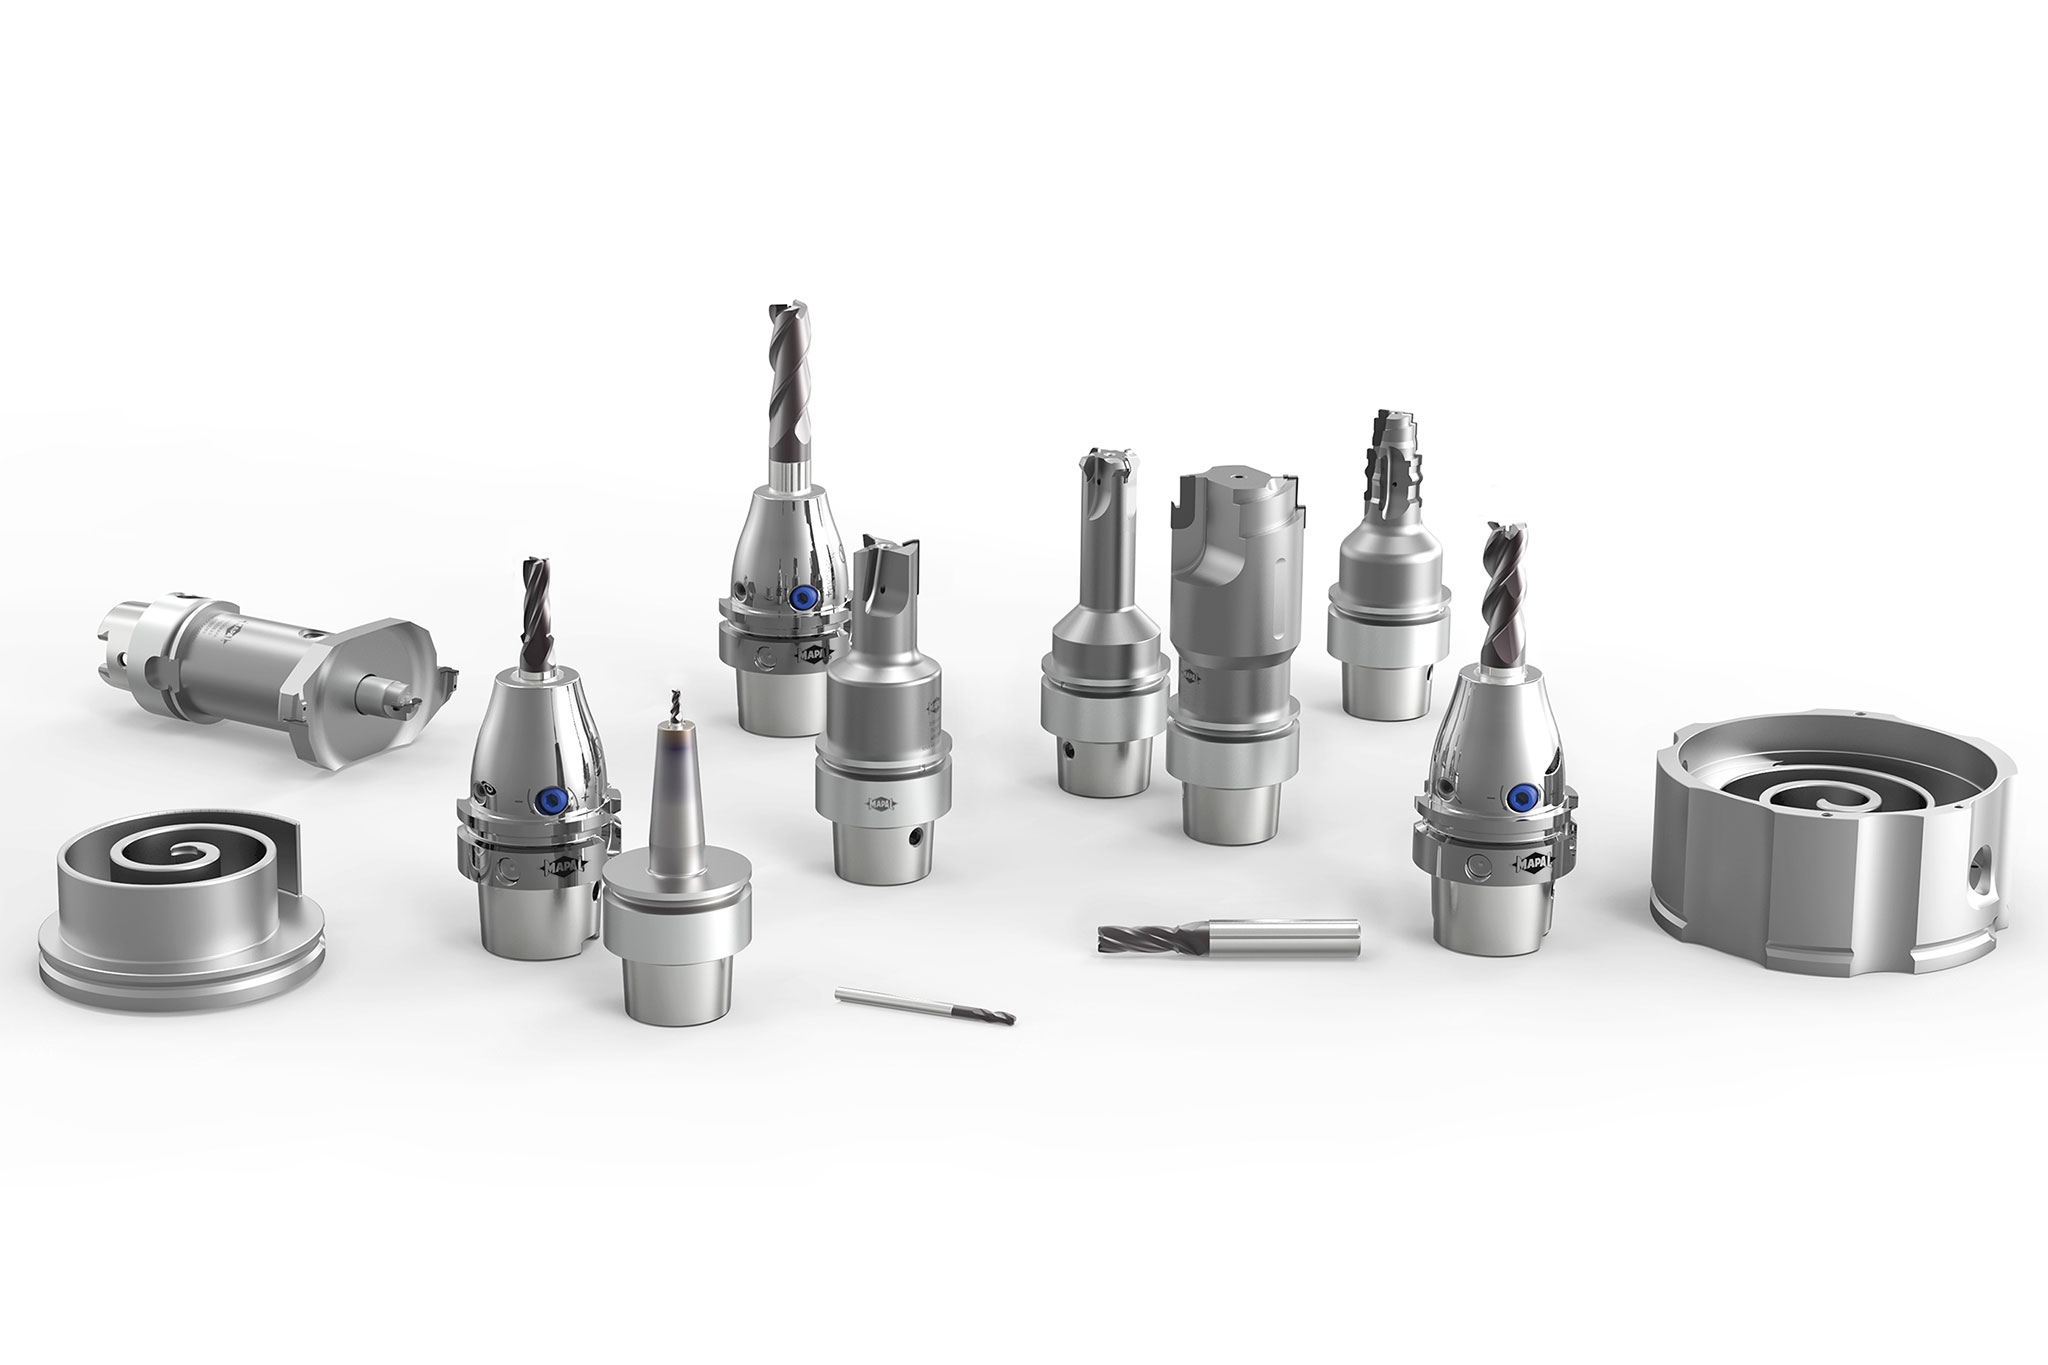
Hydrodehnspannfutter mit HSK-E sind die erste Wahl
As a full-range supplier, MAPAL maps the entire process including cycle time calculation and cutting data. The tool package includes not only the milling cutter for machining the spirals but also all the other tools for the compressor. The tool manufacturer offers the corresponding clamping device depending on the machine and spindle connection – the hydraulic chuck HSK-E is the first choice here.
Thanks to its knowledge of the market, MAPAL can keep an eye on future developments. New refrigerant specifications in the EU could result in the widely used R1234yf coolant being replaced with propane or CO2. CO2 in particular has substantial effects on the component: the displaced volume becomes much smaller and the pressure increases significantly. Current developments thus point to the use of grey cast iron or spheroidal cast iron as the material of choice for the scroll spirals, which would correspondingly affect the machining process and tool concept. With its wide range of products and technology expertise, MAPAL is ideally positioned to react to these developments quickly and offer application-specific process solutions.
Kontakt
Kathrin Rehor Public Relations Kathrin.Rehor@mapal.com Tel.: +49 7361 585 3342